Replacing a damaged quarter panel requires more than simply fitting the new panel into place—the welds must reproduce a strong, controlled joint without excessive heat distortion.
Learning how to spot weld quarter panel helps create factory-style attachment points while keeping the surrounding sheet metal properly aligned.
Incorrect weld spacing, insufficient clamping, excessive current, or poor surface preparation can cause weak joints, panel warping, and unnecessary rework during body repair.
This is especially important because quarter panels are large structural body components that must maintain accurate fitment and clean transitions with adjacent panels.
Using the correct spot-welding equipment, settings, electrode access, and weld sequence makes the repair more consistent and easier to finish.
The following guide explains the key preparation and welding considerations for achieving secure, clean spot welds when installing a replacement quarter panel.
Understanding Spot Welding For Quarter Panels
Spot welding uses electrical current to join two pieces of metal at small points. It’s often used in car manufacturing because it forms solid, reliable joints quickly. When replacing a quarter panel, spot welding helps restore the original strength and appearance.
Unlike seam welding, spot welding does not leave a continuous bead—only small, round welds at intervals. This matches the factory look and avoids warping the thin sheet metal.
Quarter panels are large body sections on the side of a car, usually covering the area from the rear door to the trunk. They’re essential for the car’s structure and appearance. Replacing or repairing a quarter panel often involves removing the damaged part and welding a new one in place.
Preparing For Spot Welding
Before you start welding, preparation is critical. Good prep makes the job easier and safer.
Tools And Materials
You’ll need:
- Spot welder (handheld or stationary)
- Quarter panel replacement piece
- Welding helmet and gloves
- Angle grinder or sander
- Drill with metal bits
- Clamps or locking pliers
- Welding primer (zinc-based for rust protection)
- Measuring tape and marker
Safety Precautions
Spot welding uses high voltage and heat. Always wear protective gear, including a helmet, gloves, and long sleeves. Make sure your workspace is clear and well-ventilated. Never weld near flammable materials.
Removing The Old Quarter Panel
Removing a quarter panel requires patience and precision.
- Mark the Cut Line: Use tape and a marker to outline where you’ll cut.
- Cut Away Damaged Metal: Use an angle grinder or cutoff wheel. Follow your marks carefully.
- Remove Spot Welds: Factory panels are usually spot welded. Use a spot weld drill bit to remove old welds without damaging the underlying structure.
- Clean Edges: After removing the panel, use a grinder to smooth rough areas.
Here’s a comparison of two removal methods:
| Method | Precision | Speed | Best For |
|---|---|---|---|
| Spot Weld Drill Bit | High | Moderate | Factory spot welds |
| Angle Grinder | Moderate | Fast | Large damaged areas |
Fitting The New Panel
Test-fit the new quarter panel before welding. Align it with body lines and clamp it in place. Check gaps and adjust as needed—good fitment prevents problems later.
Preparing Metal For Spot Welding
Proper metal prep is one of the most overlooked steps. Many beginners skip cleaning or priming, which leads to weak welds and rust.
Cleaning And Priming
- Remove Paint and Rust: Use a grinder or sanding disc to clean both surfaces where you’ll weld. Bare metal is essential.
- Apply Welding Primer: Zinc-based primer protects from rust. Spray a thin layer on the inside surfaces before assembly. Avoid painting areas where the weld will be.
Drilling Weld Holes
If your replacement panel does not have factory holes, drill weld holes every 1–2 inches along the flange. Use a 1/4″ drill bit. The holes allow the spot welder to reach both layers of metal.
Here’s a simple table comparing hole spacing:
| Spacing | Strength | Appearance |
|---|---|---|
| 1 inch | High | Factory-like |
| 2 inches | Moderate | Less visible |
| 3+ inches | Low | Not recommended |
Pro tip: Always drill holes slightly larger than the spot welder electrode tip for maximum contact.
Setting Up Your Spot Welder
Choosing the right spot welder and setting it up correctly is essential for quality results.
Types Of Spot Welders
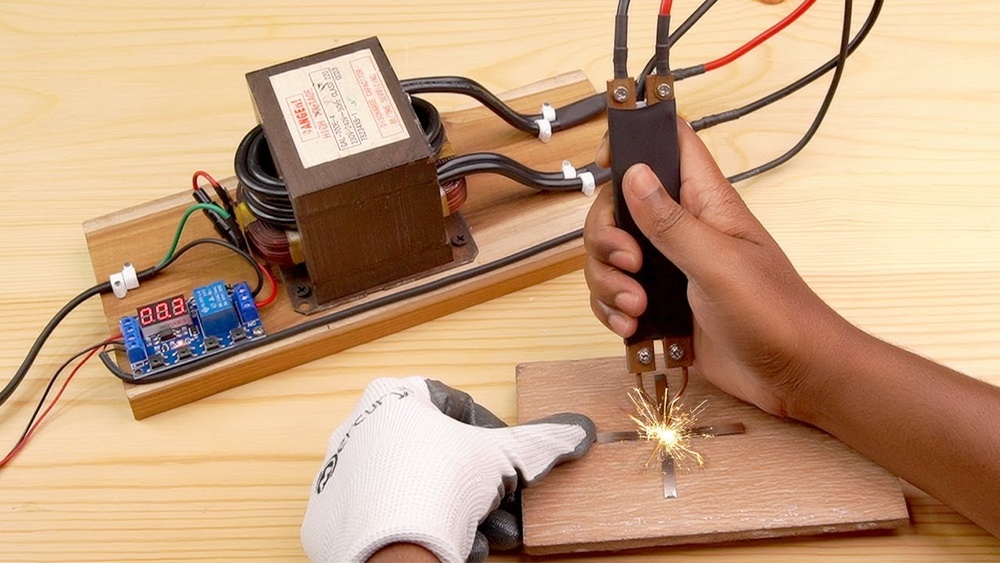
- Handheld Spot Welders: Portable, good for small jobs and tight spaces.
- Stationary Spot Welders: Larger, more powerful. Used in shops for consistent results.
Most auto body shops use handheld spot welders for quarter panels. They’re easier to maneuver and don’t require moving the car.
Adjusting Settings
- Amperage: Higher for thicker panels, lower for thin sheet metal.
- Time: Usually 1–2 seconds per weld.
Always test settings on scrap metal before starting. Adjust until you see a clean, round weld nugget with no burn-through.
Electrode Maintenance
Clean electrodes regularly. Dirty electrodes cause weak welds and can leave burn marks. Use a wire brush or dedicated cleaner.

Credit: collisionblast.com
Step-by-step Spot Welding Process
Now you’re ready to start welding. Follow these steps for a strong, factory-quality joint.
1. Position The Panel
Clamp the new quarter panel tightly in place. Check alignment and gaps. Make sure the drilled holes line up with the underlying flange.
2. Start Welding
Place the spot welder electrode tip in the first hole. Press firmly and trigger the welder. Hold for the recommended time. Release and move to the next hole.
Continue along the flange, spacing welds about 1–2 inches apart.
3. Check Weld Quality
After every few welds, inspect the joints. Look for:
- Clean, round weld nugget
- No burn-through or excessive heat marks
- Panel remains flush and aligned
4. Work In Sections
Don’t try to weld the entire panel in one go. Work in small sections, allowing metal to cool. This prevents warping.
5. Finish And Clean Up
Once all welds are complete, remove clamps. Use a grinder to smooth welds if needed. Wipe down the area and check for gaps.
Spot Welding Results: Factory Vs Aftermarket
| Result Type | Strength | Appearance | Durability |
|---|---|---|---|
| Factory Spot Weld | High | Clean, round | Long-lasting |
| Aftermarket Spot Weld | Varies | Round, sometimes uneven | Depends on prep |
Common Mistakes And How To Avoid Them
Many beginners make mistakes that can ruin the job or lead to rust. Here’s how to avoid them.
Skipping Metal Prep
Dirty or painted metal won’t weld properly. Always clean and prime.
Poor Fitment
If the panel doesn’t fit tightly, welds will be weak, and gaps will show. Test-fit multiple times.
Wrong Settings
Too much heat burns through metal; too little creates weak welds. Always test settings.
Welding Too Fast
Rapid welding overheats the metal, leading to warping. Work slowly in sections.
Ignoring Rust Protection
Spot welds expose bare metal. After welding, apply primer and seam sealer to prevent rust.
Advanced Tips For Professional Results
Even seasoned welders can improve their results with these tips.
Use Seam Sealer
After welding, apply seam sealer along the joint. This prevents water and rust.
Paint Over Welds
Once primer and sealer are dry, paint over the welded area. Match the car’s color for a factory look.
Quality Checks
Tap welded joints with a hammer. Listen for a solid sound—hollow or rattling means a weak weld.
Spot Weld Vs Plug Weld
Some repair manuals recommend plug welds (using a MIG welder) instead of spot welds. Plug welds are similar but use a filler wire. Spot welds are preferred for original appearance and strength.
Practical Example: Replacing A Quarter Panel On A Sedan
Let’s look at a real-world example. A 2010 sedan has a damaged quarter panel due to a collision.
- Prep: Remove the old panel using a spot weld drill bit. Clean and prime the replacement panel.
- Fit: Clamp the new panel in place. Check alignment with the rear door and trunk.
- Weld: Use a handheld spot welder. Weld every 1.5 inches along the flange.
- Check: Inspect each weld. Grind down rough spots.
- Finish: Apply seam sealer, primer, and matching paint.
This process restores the original look and strength of the car.

Credit: yeswelder.com
Cost And Time Estimates
Spot welding a quarter panel takes time and resources. Here are typical estimates:
- Time: 4–8 hours, depending on skill and panel size
- Cost: $200–$800 for parts and tools
Professional shops may charge $1,000–$2,500, including labor and paint.
Spot Welding Vs Other Methods
Some people use MIG welding or adhesives. Here’s a quick comparison:
| Method | Strength | Appearance | Best Use |
|---|---|---|---|
| Spot Welding | High | Factory-like | Quarter panels |
| MIG Welding | High | Visible bead | Structural repairs |
| Adhesives | Moderate | Invisible | Non-structural panels |
Key insight: Spot welding is the best choice for quarter panels because it matches factory construction and avoids visible seams.
Essential Safety Reminders
Never forget safety when spot welding. Electrical shock and burns are real risks.
- Always wear a welding helmet and gloves
- Keep fire extinguisher nearby
- Work in a well-ventilated area
- Avoid working near fuel lines or electrical wires
Two Non-obvious Insights
- Electrode Pressure Matters: Many beginners focus only on amperage and time. But the pressure applied by the spot welder electrode is just as important. Too little pressure leads to weak welds; too much can deform the panel. Always press firmly, but not excessively.
- Panel Overlap: Where the quarter panel overlaps with other body parts (like the wheel arch), slightly increasing weld spacing can prevent stress cracks. Factories often use variable spacing for this reason.
Maintaining Your Spot Welder
Regular maintenance ensures consistent results.
- Clean electrodes after every job
- Check cables for wear
- Lubricate moving parts
A poorly maintained welder leads to inconsistent welds and can fail during critical repairs.
When To Seek Professional Help
If you’re unsure about panel fitment, weld quality, or rust protection, consider asking a body shop for advice. Some shops may spot weld your panel for a small fee if you prep and fit it yourself.

Credit: www.youtube.com
Wrapping Up
Spot welding a quarter panel is a skill worth mastering for anyone interested in car restoration or repair. With the right tools, careful preparation, and attention to detail, you can achieve professional results that last for years. Always focus on safety, quality, and fitment—and remember, every weld counts.
Frequently Asked Questions
What Is Spot Welding And Why Is It Used On Quarter Panels?
Spot welding is a process where two pieces of metal are joined at small points using electrical current. It’s used on quarter panels because it creates strong, clean joints without warping the sheet metal. This matches the factory look and preserves the car’s structure.
How Many Spot Welds Should I Use For A Quarter Panel?
Most manufacturers recommend one weld every 1–2 inches along the flange. Too few welds can weaken the panel, while too many can cause overheating and distortion.
Can I Spot Weld Over Painted Or Rusty Metal?
No. Always clean metal surfaces before spot welding. Paint or rust stops the electrical current and leads to weak, unreliable welds.
What Should I Do If A Spot Weld Fails?
If a spot weld doesn’t hold, grind it out and redo the weld. Make sure both surfaces are clean, the welder settings are correct, and you’re applying enough pressure with the electrode.
Is Spot Welding Safe For Beginners?
Yes, but you must follow safety precautions. Wear protective gear, keep your workspace clear, and never weld near flammable materials. Practice on scrap metal before working on your car.